Leave Your Message

How to Source 18650 Cylindrical Battery Pilot Line in 2026?

Sourcing an 18650 Cylindrical Battery Pilot Line in 2026 requires more than comparing equipment prices. It requires a practical understanding of process control, cell safety, supplier capability, and future production goals. The line should support repeatable electrode coating, accurate slitting, stable winding, controlled electrolyte filling, formation, aging, and final testing.

Professor Shirley Meng has emphasized a useful manufacturing principle: “Battery innovation is not only about chemistry; it is also about manufacturing.” This idea matters when evaluating pilot-line suppliers. A strong laboratory cell may fail during scale-up if coating thickness varies, welding creates excessive resistance, or formation data lacks traceability.

Look closely at the physical workflow. Can the coating machine maintain uniform loading across a narrow electrode roll? Are dry rooms properly specified for moisture control? Does the winding station protect separator alignment at high tension? Ask suppliers to demonstrate real process data, not only polished brochures. Review sample inspection records, equipment acceptance criteria, service response times, and operator training plans.

The best 18650 Cylindrical Battery Pilot Line is rarely the cheapest option. It should provide flexible recipe control, safe handling, reliable data collection, and room for process learning. That last point is often underestimated.

No shortlist is perfect. A supplier may have excellent hardware but weak technical support. Another may offer strong engineering but limited delivery experience. Buyers should test both claims through reference visits, sample trials, and detailed factory-acceptance discussions. In 2026, careful sourcing means choosing a line that can reveal problems early, before they become expensive production habits.

How to Source 18650 Cylindrical Battery Pilot Line in 2026?

Define the 18650 Cell Spec: 18×65 mm, 3.6–3.7 V, 2.5–3.5 Ah

How to Source an 18650 Cylindrical Battery Pilot Line in 2026?

The 18650 designation defines a cylindrical cell near 18 mm in diameter and 65 mm in length. In practice, the finished size can change slightly with insulation, wrapping, and manufacturing tolerance. Your fixture must allow clearance. A tight drawing can create expensive assembly problems.

Set the nominal voltage at 3.6–3.7 V, depending on the selected chemistry and supplier documentation. The 2.5–3.5 Ah range also needs careful definition. Capacity alone is not enough. Record discharge current, test temperature, cutoff voltage, cycle-life target, and capacity tolerance. A cell rated at 3.5 Ah may perform differently under a high-current load. Ask for test reports from controlled samples, not only a product sheet.

For a pilot line, verify incoming cells with dimensional checks, open-circuit voltage, internal resistance, and capacity testing. Use calibrated instruments and retain sample records by production lot. The welding process should match the cell tab material and heat limits. Excessive heat can damage the separator, even when the casing looks normal. I have seen teams focus heavily on capacity and overlook storage conditions. That mistake can distort early results. The specification should also define protection requirements, labeling, traceability, and transport packaging. Leave realistic tolerance bands. Perfect numbers rarely survive real production.

Set Pilot-Line Capacity Targets: 10–100 MWh/Year and 100% Traceability

A 10–100 MWh annual target gives an 18650 pilot line a practical development range. At 3.6 V and 3.2 Ah per cell, 10 MWh equals roughly 870,000 cells yearly. The 100 MWh level approaches 8.7 million cells. Chemistry changes this estimate. So does scrap rate.

The International Energy Agency reported that global electric-vehicle battery demand exceeded 750 GWh in 2023. Its Global EV Outlook 2024 also shows continued capacity expansion through 2035. A pilot line should therefore test repeatability, not only maximum speed. Specify formation capacity, usable yield, changeover time, and quarantine space. A 10 MWh line may suit process validation, while 100 MWh supports customer sampling and early qualification. Do not treat nominal capacity as sellable output.

Traceability must cover every cell. Record electrode-lot numbers, coating weight, calendering thickness, winding tension, electrolyte batch, weld parameters, formation curves, and final electrical results. Use a time-stamped digital record linked to each cell’s barcode. The EU Battery Regulation introduces battery-passport obligations for relevant batteries from 2027, making data discipline commercially important. Industry quality guidance also favors measured process capability over verbal assurances. Keep raw records accessible.

A weak point remains obvious: 100% traceability does not guarantee 100% data accuracy. Sensors drift. Operators enter incorrect codes. Pilot teams should audit records daily, verify barcode links, and physically reconcile samples. Design the line for controlled learning, not impressive brochures.

Select Equipment for Coating, Winding, Welding, Filling, and Formation

How to Source an 18650 Cylindrical Battery Pilot Line in 2026

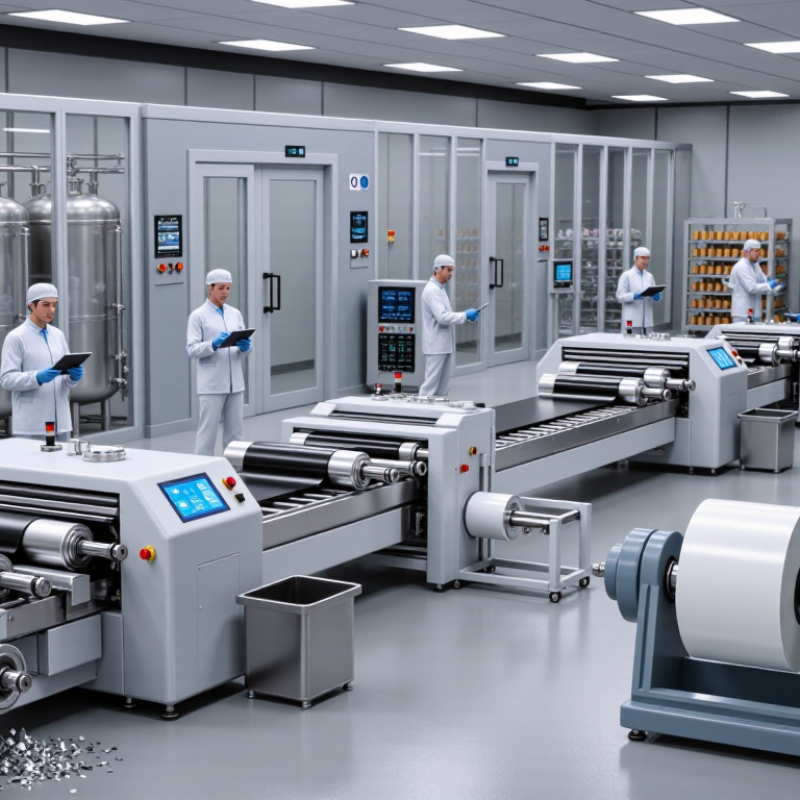
Selecting a pilot line for 18650 cells requires more than comparing equipment prices. Start with the coating unit. Check slurry viscosity control, web tension, drying-zone temperatures, and electrode thickness accuracy. A stable coating profile reduces later defects. Ask suppliers for measured data, not only catalog limits. Include an inspection camera and a practical method for sampling coated electrodes.

Winding equipment should control alignment, tension, and separator handling without damaging thin materials. Welding systems need repeatable tab joints, low spatter, and traceable weld parameters. Small variations matter. During electrolyte filling, specify vacuum control, filling accuracy, chamber cleanliness, and compatible sealing methods. The dry room must support the required moisture level, with records linked to each batch. Poor humidity control can create problems that appear much later.

Formation and aging equipment deserve equal attention. Choose channels with independent voltage and current control, temperature monitoring, safety interlocks, and exportable test data. A pilot line should allow recipe changes without complicated downtime. I would also request factory acceptance tests using realistic materials, because demonstrations often use ideal samples. One lesson worth revisiting is equipment integration: excellent machines can still fail as a system. Leave space for maintenance, rejected cells, calibration, and operator movement. Documentation, training, spare parts, and service response should be evaluated beside technical performance, not after installation.

Qualify Suppliers Against IEC 61960, IEC 62133-2, UN 38.3, and UL 1642

Sourcing an 18650 cylindrical battery pilot line in 2026 requires evidence, not attractive capacity claims. Ask each supplier for a documented qualification plan against IEC 61960, IEC 62133-2, UN 38.3, and UL 1642. IEC 61960 helps verify capacity, discharge performance, dimensions, marking, and consistency. IEC 62133-2 focuses on safety during charging, discharging, vibration, shock, and abnormal use. Request the exact test edition, laboratory identity, sample configuration, and report scope.

UN 38.3 is essential for transport approval. Review the test summary and confirm it matches the proposed cell design. Do not accept a report for an older chemistry or different vent structure. UL 1642 evidence should cover the cell construction, insulation, protection features, and abuse testing. A pilot supplier should also show lot traceability, incoming inspection, welding parameters, formation records, and quarantine procedures. Check capacity distribution and internal resistance from real pilot data. One impressive sample proves very little.

Tips: Visit the line if possible. Watch formation racks, aging rooms, and visual inspection. Ask operators to explain failure handling. Request three pilot lots, not one. Compare voltage, mass, capacity, and resistance across lots. Small gaps matter. I would record every unanswered question, even if the supplier seems technically strong. Some qualification decisions become clearer after a difficult meeting.

How to Source an 18650 Cylindrical Battery Pilot Line in 2026?

Supplier Qualification Against IEC 61960, IEC 62133-2, UN 38.3, and UL 1642

This qualification map shows the primary scope of each standard for an 18650 pilot-line supplier. A value of 1 indicates that the topic is directly addressed by the standard, while 0 indicates that it is not the standard’s primary purpose. IEC 61960 focuses on performance and marking, IEC 62133-2 on portable lithium-cell safety, UN 38.3 on transport testing, and UL 1642 on lithium battery cell safety. Final supplier approval should verify the applicable edition, test reports, construction review, traceability records, and production-control evidence.

Audit Pilot-Line Economics: Yield, Energy Density, OEE, Lead Time, and MOQ

How to Source 18650 Cylindrical Battery Pilot Line in 2026?

A pilot line should be priced through usable cells, not installed equipment. During factory audits, request yield data from electrode coating through final testing. A 92% final yield can become 86% after formation losses and rework. Small gaps matter. Model scrap, labor, utilities, maintenance, and electrode material separately. One spreadsheet is rarely enough.

Energy density must match the target chemistry, loading, and cycle-life requirement. Ask for measured Wh/kg from production samples, not laboratory projections. Inspect coating thickness maps, winding tension records, electrolyte filling controls, and formation curves. OEE also needs evidence. Review availability, performance speed, and quality losses across several shifts. A line running at 70% OEE may look attractive, but its effective output can disappoint.

Lead time includes design approval, component procurement, installation, commissioning, and operator training. Set acceptance milestones with measurable yield and capacity conditions. MOQ deserves equal attention. A low trial quantity may carry higher unit costs, while a large MOQ can trap cash in unused materials. Our early cost model underestimated changeover time by nearly 30%. That mistake exposed weak scheduling assumptions. Request a ramp plan, spare-parts list, calibration records, and training logs. Confirm local service capability and documented compliance with applicable battery transport, worker-safety, and environmental requirements. Audit the evidence, not the promise.

How to Source 18650 Cylindrical Battery Pilot Line in 2026? - Audit Pilot-Line Economics: Yield, Energy Density, OEE, Lead Time, and MOQ

Practical sourcing benchmark for a small-format 18650 lithium-ion cell pilot line. Values are planning ranges for supplier comparison and technical due diligence, not company-specific quotations.

Audit Dimension Unit Typical Pilot-Line Range Recommended 2026 Planning Assumption What to Verify During Supplier Audit Economic Impact
Cell format mm 18 × 65 cylindrical format 18.0–18.5 mm diameter; 64.5–65.5 mm height Can the winding, grooving, crimping, testing, and formation fixtures maintain dimensional tolerances without frequent manual adjustment? Medium
Typical pilot capacity cells/year 50,000–500,000 150,000–250,000 finished cells/year Confirm rated capacity at the agreed product mix, shift pattern, planned maintenance, and first-pass yield rather than nameplate speed. High
Nominal voltage V 3.6–3.7 3.6 V for conservative energy calculations Check the voltage definition used in datasheets and whether energy calculations use nominal voltage or the full discharge curve. Medium
Typical cell capacity Ah 2.0–3.5 2.5–3.2 Ah for a new pilot design Review capacity distribution, test current, charge/discharge limits, temperature, and end-of-discharge voltage. High
Cell-level gravimetric energy density Wh/kg 220–280 240–260 Wh/kg at initial pilot maturity Require complete-cell mass, measured capacity, nominal voltage, and test protocol. Exclude electrode-only or theoretical values. High
Volumetric energy density Wh/L 500–700 550–650 Wh/L Verify whether volume includes the complete cylindrical cell, insulation, safety vent, and terminal features. High
First-pass yield % 80–92% ≥88% after process stabilization Obtain yield by process step: coating, slitting, winding, assembly, electrolyte filling, formation, aging, and final grading. Very high
Stabilized yield target % 90–96% 92–94% before scale-up approval Check whether the reported figure excludes cosmetic rejects, low-capacity cells, leakage failures, and cells held for rework. Very high
Overall equipment effectiveness (OEE) % 45–70% 55–65% during pilot production Audit availability, performance, and quality separately. Request downtime logs, changeover records, minor-stop data, and actual cycle times. Very high
Coating-line speed m/min 5–30 10–20 m/min for development-scale production Confirm usable speed at the required coating weight, edge quality, drying profile, solvent recovery, and electrode loading. Medium
Electrode loading variation % from target ±1.5–3.0% ≤±2.0% across production width Review cross-web and machine-direction measurements, sampling frequency, weighing method, and control limits. High
Electrode moisture before assembly ppm Typically ≤300–500 Set a chemistry-specific limit, commonly ≤300 ppm for moisture-sensitive lithium-ion processes Verify Karl Fischer testing, dry-room dew point, transfer time, material hold time, and calibration records. High
Dry-room dew point °C −35 to −50 −40 °C or lower in assembly and electrolyte-filling areas Check actual dew-point mapping at operator stations, door openings, maintenance events, and material entry points. High
Formation and aging duration hours 24–96+ per batch 48–72 hours for initial economic modeling Review charge protocol, rest periods, aging temperature, rack capacity, grading rules, and whether formation equipment is the bottleneck. Very high
Formation energy consumption kWh per kWh of cell output 0.08–0.25 0.12–0.18 Ask whether the figure includes charger losses, HVAC, dry-room loads, compressed air, cooling water, and recovery of discharge energy. Medium
Total electricity intensity kWh per kWh of cell output 1.5–4.0 2.0–3.0 for a small pilot line Separate process electricity from facility overhead and validate with utility meters rather than calculated equipment ratings. High
Indicative pilot-line equipment CAPEX USD $0.8–3.0 million $1.2–2.0 million, excluding building purchase and major upstream material plants Request a line-item quotation covering coating, drying, calendaring, slitting, winding, assembly, filling, formation, aging, testing, utilities, installation, and commissioning. Very high
Facility and utility preparation USD $0.3–1.5 million $0.5–1.0 million depending on existing infrastructure Include dry-room HVAC, fire protection, exhaust, solvent handling, nitrogen, chilled water, compressed air, electrical service, and battery safety systems. Very high
Pilot-line labor requirement FTE per shift 8–20 12–16 FTE per operating shift Count operators, maintenance, quality, process engineering, material handling, and shift supervision; do not count only machine operators. High
Indicative conversion cost USD/kWh $25–80 $35–60/kWh during early pilot operation Confirm whether conversion cost includes labor, utilities, consumables, scrap, depreciation, maintenance, quality testing, and facility overhead. Very high
Material scrap and loss % of input material 5–20% 8–12% after process stabilization Track scrap separately for coating trim, slitting, winding defects, assembly damage, electrolyte loss, formation rejects, and final grading. Very high
Equipment manufacturing lead time weeks 12–24 16–20 weeks after technical specification approval Identify long-lead components, acceptance-test milestones, software completion, spare-parts availability, and change-order impact. High
Installation and commissioning weeks 4–10 6–8 weeks after site readiness Confirm installation responsibility, utility connection dates, dry-room qualification, safety validation, operator training, and trial-production support. High
Time to first qualified cell weeks from purchase order 20–36 24–32 weeks Define “qualified cell” using capacity, internal resistance, leakage, dimensional, safety, cycle-life, and consistency criteria. Very high
Minimum order quantity for equipment line or lot 1 complete pilot line or defined module Buy by process module only when interfaces and controls are standardized Check whether partial-line orders preserve warranty, software integration, process responsibility, and performance guarantees. Medium
Minimum order quantity for pilot cells cells per lot 1,000–10,000 3,000–5,000 cells for initial process validation Confirm whether the supplier can provide traceability by electrode lot, winding batch, electrolyte batch, formation recipe, and test grade. Medium
Recommended acceptance batch cells 500–2,000 At least 1,000 cells across multiple production lots Use statistically meaningful sampling and require raw test data instead of average values only. High
Internal resistance consistency coefficient of variation ≤10–15% for a mature pilot process ≤12% within the same grade and test condition Standardize measurement temperature, SOC, rest time, AC/DC method, fixture resistance, and data filtering. High
Early cycle-life target cycles to retained capacity 500–1,000 cycles to 80% capacity, chemistry dependent Use 800 cycles to 80% as an initial screening target Specify charge rate, discharge rate, temperature, voltage window, rest period, sample size, and failure definition. Very high
Quality-system readiness audit status Documented process controls and traceability required Process FMEA, control plan, calibration system, nonconformance process, and lot-level traceability active before ramp-up Audit document revision control, gauge calibration, corrective-action closure, change management, and electronic data retention. High
Commercial sourcing decision gate decision rule Do not approve on price alone Approve only when yield, OEE, safety, lead time, and total installed cost meet the agreed thresholds Use a weighted scorecard: 25% yield and quality, 20% process capability, 20% total cost, 15% lead time, 10% service, and 10% flexibility. Very high
Benchmark note: The ranges above are engineering planning benchmarks for 18650 lithium-ion pilot production. Actual results vary with cathode and anode chemistry, electrode loading, cell design, automation level, product qualification criteria, facility conditions, labor rates, utility prices, and local safety requirements. All supplier quotations should be normalized to the same capacity, yield, OEE, warranty, installation scope, testing protocol, and acceptance criteria.